In CNC machining, holes are some of the simplest features in CNC machined parts. They can be tricky sometimes to machine because the cutting tool has to work inside a confined space, where access, chip removal, heat, and tool rigidity are all in one place.
Design choices like depth, hole types, diameter, and placement can affect accuracy, machining time, and cost. Knowing CNC machining holes and when exactly to use each one makes it easier to design parts. In this article, we cover common types of CNC machining holes, how to choose the Right Hole, and common CNC Hole Design Mistakes.
Common Types of CNC Machining Holes
CNC machining parts often involves holes: through-holes, blind holes, and tapered holes are common. There are a few more practical types worth knowing.
Some holes provide clearance for fasteners, and some align mating parts with pins, carry fluid, and create a threaded connection. Although we often talk about drilling holes and only one way to make them, CNC holes might be drilled, interpolated with an end mill.
Here are the most common types,
Through Holes
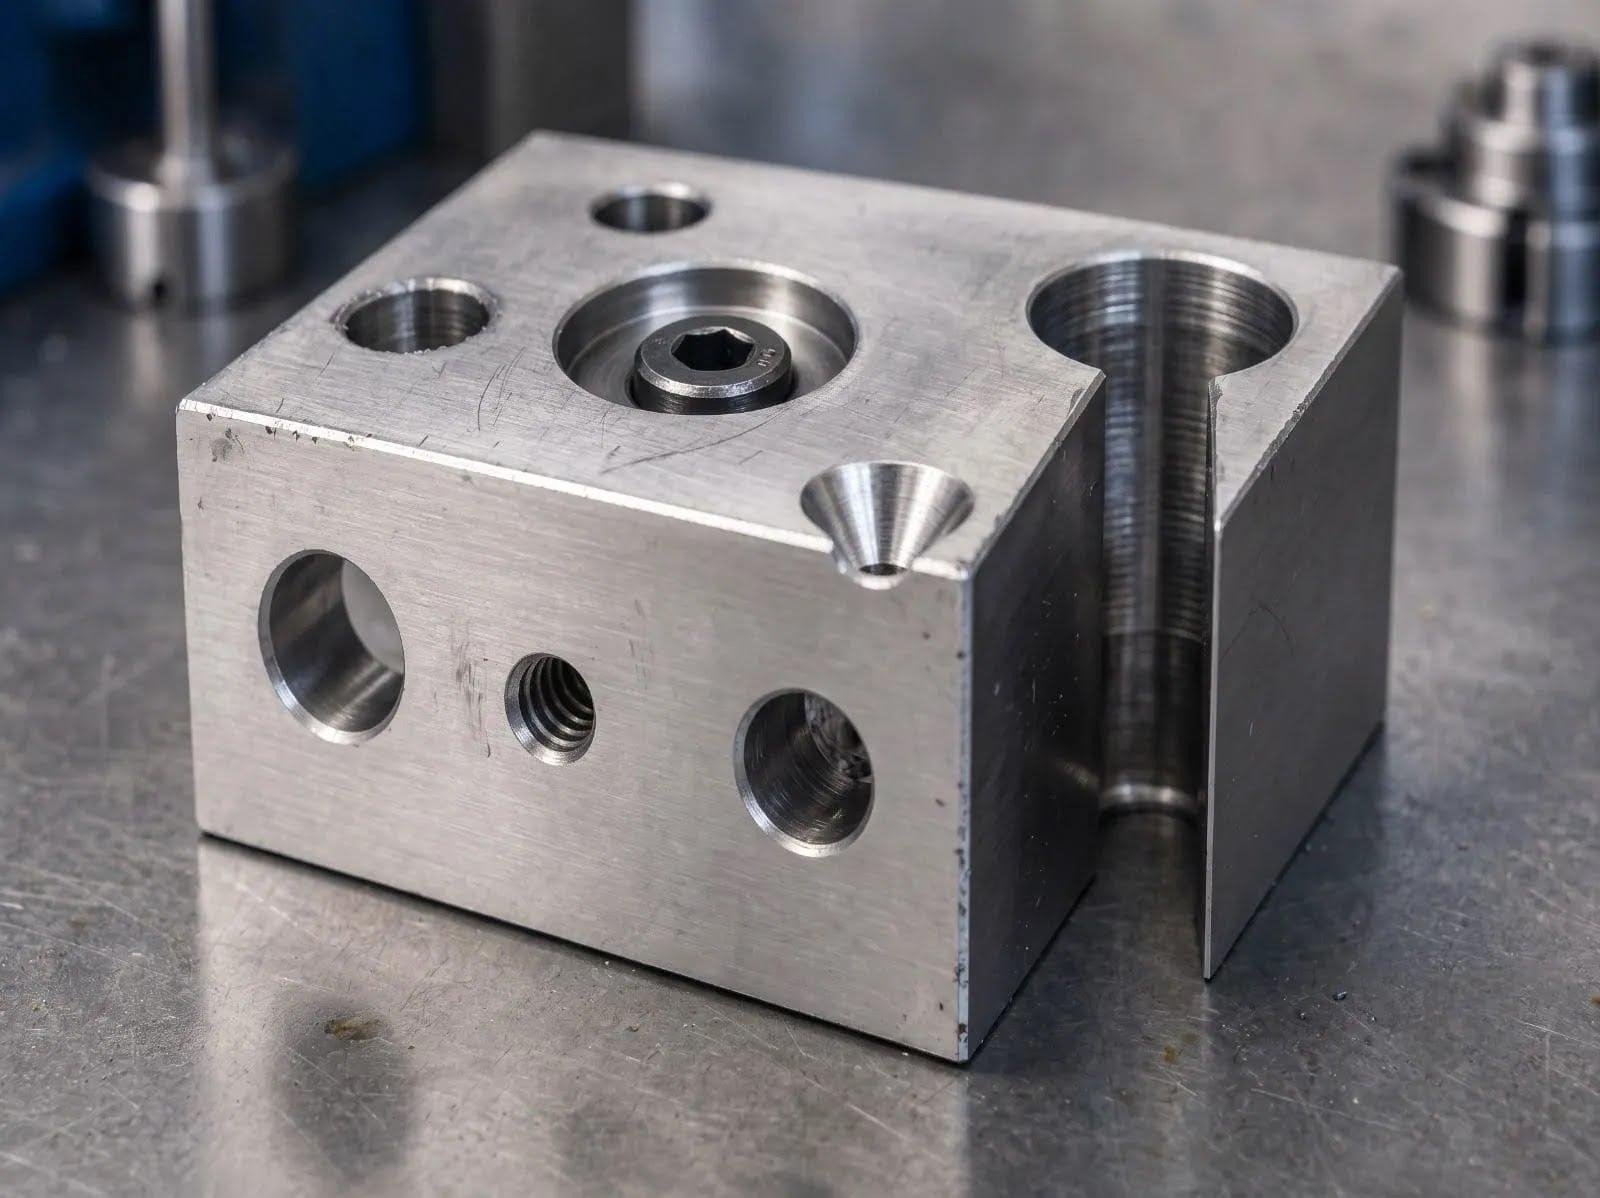
Through hole simple to undersand, its extends completely through the part. These hole usually considered the simplest holes to machine because the tool can pass all the way through, and chip removal is easier for the machine. Through holes are commonly used for clearance, alignment features, fluid passages, and weight reduction. If your application allows, then it’s an easier option to consider.
Blind Holes
A blind hole stops before reaching the opposite side. Useful when one surface needs to stay intact. A little bit difficult because chips simply can’t exit through the end, machining work a little bit more.
Tapped (Threaded) Holes
Tapped hole or threaded hole internal female threads so a scew can fasten directly into the part. Specifically, only the thread depth the connection needs, since extra depth can drive up machining time. Internal threads can be cut with a thread mill rather than a traditional tap, allowing one tool to cut multiple thread sizes that share the same pitch, and it may reduce setup time in some setups.
Reamed Holes
A reamed hole comes into play when a standard machined hole doesn’t provide the required size control. The hole is made slightly undersized first, then a reamer removes a small amount of material to bring it to its final size. Reamed holes are often used for dowel pins, precision shafts, bearings, and alignment features. Also note that reaming adds another operation, which means some extra cost, so only use it when your application demands and needs precision.
Counterbore Holes
A counterbore adds a larger cylindrical recess above a smaller hole, and this lets socket-head cap screws and similar fasteners sit flush with or below the part surface. So, the head doesn’t interfere with other components.
Countersink Holes
A countersink uses a conical recess instead of a cylindrical one. It’s designed for flat-head screws that need to sit flush with the surrounding surface. Just make sure the angle matches the fastener you are using, since most common standards include 82°, 90°, and 100°.
How to Choose the Right Hole Feature
When you are at the design stage and considering hole features, consider fastener type, required fit, material thickness, tooling, and tolerance. Choose a hole according to application requirements. Use a simple feature that meets the functional requirements. Simple hole designs are generally faster to machine and easier to inspect.
| Reason | Hole Type | Why |
| Pass a fastener through a part | Through hole | Usually the simplest option when the hole can extend through the part |
| Thread directly into the part | Tapped hole | Eliminates the need for a separate nut |
| Recess a socket-head fastener | Counterbore | Lets the fastener head sit flush with or below the surface |
| Flush-mount a flat-head screw | Countersink | Matches the tapered head of the fastener |
| Achieve precise alignment | Reamed hole | Provides tighter diameter control and a smoother finish |
| Keep the opposite surface intact | Blind hole | Stops the hole before it passes through the part |
Common Mistakes to Avoid
Common issues with CNC parts machining holes come from unnecessary adding more depth, add more complexity than required, extra precision feature actually needs. For a CNC machining parts manufacturer, tighter tolerances may require additional machining, inspection, and quality-control time.
Common reason:
- Specifying blind holes deeper than needed
- Choosing nonstandard fastener sizes without a functional reason
- Applying tight tolerances to non-critical features
- Positioning holes too close to part edges
- Forgetting to specify countersink angles
- Calling for more thread depth than needed
- Designing features with poor tool access
Conclusion
Choosing the right hole type for your application makes CNC machining easier and helps avoid unnecessary work. Start with what the part needs, then use the simplest hole feature that gets the job done.